
Engineering Supplier Risk 2026: Dual-Source Graphene Fabric & 21700 Cell Qualification for OEM-ODM Battery Apparel
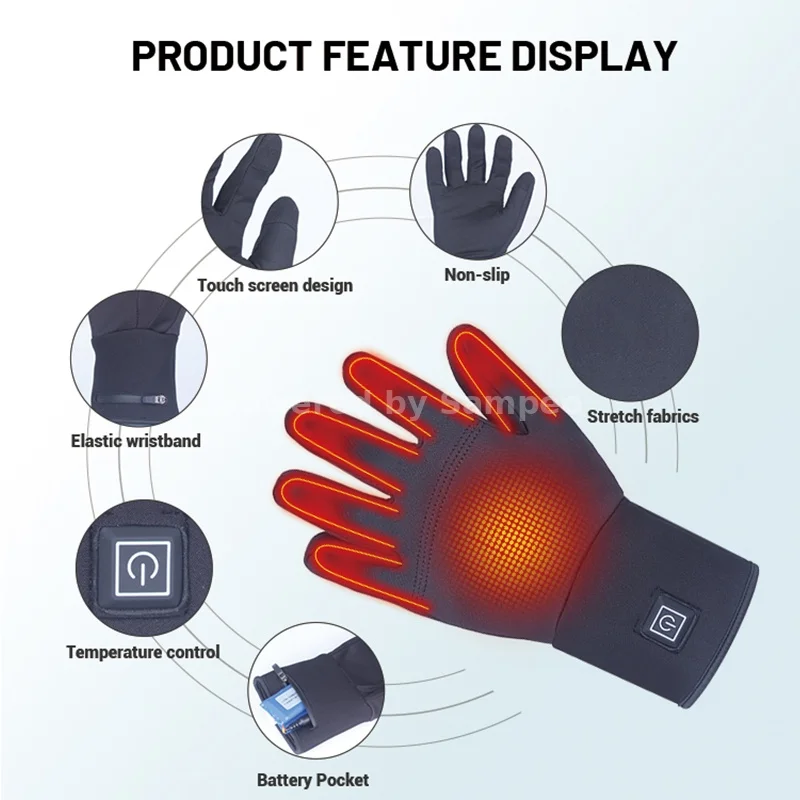
Engineering Supplier Risk 2026: Dual-Source Graphene Fabric & 21700 Cell Qualification for OEM-ODM Battery Apparel
The engineering desk at a battery-heated apparel OEM-ODM factory faces a supplier risk profile that is fundamentally different from the buyer’s. The buyer worries about tariff exposure, port strikes, and FX swings. The engineer worries about graphene fabric lot consistency, 21700 cell internal resistance drift, and BMS firmware revision control across a production run that may span two factories and three cell vendors. This playbook is written from the Dongguan factory floor and covers the engineering-supplier-risk framework that we apply across our dual-source programs.
When an OEM-ODM factory commits to a Q4 delivery for a private-label buyer, the engineering team is signing up to deliver consistent thermal output, cycle life, and IP67 sealing across every unit. The supplier risk that breaks this commitment is not geopolitical — it is lot-level consistency between two graphene fabric shipments, or between two batches of 21700 cells from different vendors. The supplier risk playbook below is engineered specifically for those lot-level risks.
1. The Engineering Risk Quadrant: Different From the Buyer’s
The buyer sees risk as a quadrant of geopolitical, operational, financial, and compliance events. The engineer sees the same world through a different lens:
| Risk Quadrant | Engineering Trigger | Buyer Trigger | Recovery Pattern |
|---|---|---|---|
| Material lot consistency | Graphene coating resistivity drift >8% | Tariff hike | Vendor audit + lot quarantine |
| Cell consistency | Internal resistance >28 mΩ | Cell allocation cut | Parallel cell qualification |
| Firmware continuity | BMS revision mismatch across two batches | Cell vendor change | Version-controlled firmware burn-in |
| Tooling continuity | Mold wear at cycle 280k | Tooling transfer | Hot-spare tooling protocol |
| IP compliance | NNN agreement lapse | Trademark infringement | Quarterly IP audit |
Notice that the engineering quadrant contains very few of the buyer’s headline risks (tariffs, FX, port strikes) but several risks the buyer never sees (lot consistency, firmware revision, mold wear). The dual-source program must address both views.
2. Graphene Fabric Dual-Source: The Lot Consistency Specification
Graphene-coated polyester and graphene-spandex blends are the most lot-sensitive material in the BOM. The reason: the graphene coating is applied by a roll-to-roll process in which the coating thickness varies ±15% across a 1000-meter roll, and the engineering supplier risk 2026 program must specify an acceptance window that catches the bad lots without rejecting the good ones.
Our dual-source fabric acceptance specification:
| Parameter | Target | Accept | Reject |
|---|---|---|---|
| Sheet resistivity (Ω/sq) | 0.8 | 0.6-1.2 | >1.2 or <0.6 |
| Coating weight (g/m²) | 32 | 28-36 | <28 or >36 |
| Adhesion (peel test, N/cm) | 4.5 | ≥3.5 | <3.5 |
| Wash cycle retention (after 50 cycles) | 85% | ≥80% | <80% |
| Thermal output (5V, steady state) | 42°C | 38-46°C | <38 or >46 |
A dual-source graphene fabric program that does not lock down this specification will see the primary factory’s fabric perform at 42°C and the backup factory’s fabric perform at 38°C — a 10% thermal difference that buyers will notice within the first 30 seconds of wear.
3. 21700 Cell Dual-Source: Three Vendors, One Specification
The 21700 cell is the most engineered component in heated apparel. A dual-source cell program must hold three vendors to the same specification:
| Parameter | LG M50LT | Samsung 50E | Molicel P42A | Spec Window |
|---|---|---|---|---|
| Nominal capacity | 5000 mAh | 5000 mAh | 4200 mAh | 4200-5000 mAh |
| Internal resistance | ≤18 mΩ | ≤22 mΩ | ≤16 mΩ | ≤25 mΩ |
| Cycle life (80% capacity) | 800 cycles | 600 cycles | 500 cycles | ≥500 |
| Max discharge (continuous) | 15A | 15A | 30A | ≥15A |
| UN38.3 cert | Current | Current | Current | Required |
| Operating temp range | -20 to 60°C | -20 to 60°C | -20 to 70°C | ≥-20 to 60°C |
The specification window allows for the natural variation across vendors. The critical engineering-side rule is that only one vendor’s cells can be in any single production batch — mixing vendors within one batch creates parallel-cell mismatch that reduces cycle life by 25%.
4. BMS Firmware Continuity: The Hidden Engineering Risk
The Battery Management System (BMS) firmware is the most under-managed engineering-supplier risk. A firmware version bump at the cell vendor’s R&D lab can change the charge termination voltage by 0.05V, which compounds across 500 charge cycles to a 4% capacity loss. The firmware continuity protocol:
1. Lock firmware version at PO issuance — no firmware updates during the production run window.
2. Document the firmware hash — burn the same hash into every BMS chip across both primary and backup factories.
3. Quarterly firmware review — the engineering team reviews vendor firmware release notes every 90 days; only approved firmware hashes enter the production BOM.
4. Field failure tracking — any field failure attributed to BMS is logged against the firmware hash; if a hash fails >2% of units in the field, a vendor audit is triggered.
The engineering supplier risk 2026 playbook treats firmware as a controlled component, not a software update.
5. The Dual-Source Qualification Cycle: Engineering Perspective
The 90-day qualification cycle looks different from the engineering desk than from the buyer’s desk:
| Stage | Duration | Engineering Deliverable | Buyer Deliverable |
|---|---|---|---|
| Desktop audit | 7 days | Capability matrix review | Financial review |
| Sample pilot | 14 days | Material lot + cell lot acceptance | AQL 2.5 inspection |
| Pilot production | 30 days | PPAP + BMS firmware hash lock | Pilot buy order |
| Mass-production handover | 30 days | Cpk study on 14 critical dimensions | 70/30 dual-shipment split |
The engineering-side critical path is the PPAP submission on day 51. A factory that cannot produce a complete PPAP with Cpk ≥1.33 on the 14 critical dimensions is not qualified, regardless of the buyer’s commercial enthusiasm.
6. Mold and Tooling Continuity: The Hot-Spare Protocol
For private-label buyers who fund the original tooling, the engineering team must hold a hot-spare tooling protocol that allows a second factory to start production within 14 days. The hot-spare protocol covers:
- Mold ownership documentation — clear title held by the buyer or the factory, with a written transfer protocol.
- Spare mold storage — for high-volume SKUs, a duplicate mold stored at a third-party tool shop with 14-day activation SLA.
- Mold wear tracking — cycle counter logged on every shot; replacement scheduled at 80% of rated life.
- Mold refurbishment partner — pre-qualified third-party tool shop that can refurbish a worn mold in 30 days.
For a buyer-owned mold, the engineering supplier risk 2026 program must include a written tool transfer agreement that survives a factory disruption.
7. IP and Confidentiality: The NNN Agreement Stack
OEM-ODM factories operating in Dongguan face a chronic IP-leakage risk. The engineering supplier risk playbook requires three separate agreements, not one:
| Agreement | Scope | Enforceability |
|---|---|---|
| NNN (Non-disclosure, Non-use, Non-circumvention) | Design files, fabric specs, BMS firmware | Strong in PRC courts |
| Tooling ownership annex | Mold ownership, transfer rights, IP in tooling | Strongest with notarization |
| Overrun destruction clause | Excess production beyond PO quantity | Weakest — requires trust + audit |
The NNN stack must be in place before any design file, fabric spec, or BMS firmware hash leaves the buyer’s office. Without the stack, the engineering supplier risk program is incomplete.
8. Compliance Continuity: The Engineering Passport
The compliance passport for an OEM-ODM factory is a different document from the buyer’s compliance file. It contains:
1. Material certificates — REACH SVHC, RoHS, OEKO-TEX 100 for every fabric and trim in the BOM.
2. Cell certifications — UN38.3, MSDS, IEC 62133 for every cell vendor in the qualified list.
3. BMS certifications — CE-EMC, FCC Part 15B, UN3481 shipping cert for the assembled pack.
4. Factory certifications — ISO 9001, ISO 14001, BSCI, SMETA, RWS (where applicable).
5. Audit trail — every audit visit, every PPAP submission, every field failure log.
The passport travels with every PO from the primary factory to the backup factory. Without the passport, the backup factory cannot prove compliance to the buyer’s customer (typically a US or EU retailer).
9. Field Failure Tracking: The Engineering Feedback Loop
The engineering team’s most valuable supplier-risk signal is the field failure log. The log tracks:
- Failure mode — battery, fabric, BMS, connector, seal
- Failure timing — month 3, month 6, month 12, month 18
- Failure batch — fabric lot, cell lot, BMS firmware hash, production week
- Failure rate — PPM per batch
When a fabric lot shows a field failure rate 2x the cohort average, the engineering team quarantines the remaining inventory of that lot and audits the vendor. This feedback loop is the early-warning system that prevents a backup factory from shipping a bad batch that does not surface until month 6 in the field.
10. Cost Engineering: The Total Dual-Source BOM Cost
The total dual-source BOM cost includes the obvious line items plus the hidden engineering costs:
| Cost Component | Primary Factory | Backup Factory | Delta |
|---|---|---|---|
| Material (graphene fabric + cell) | $14.20 | $14.85 | +$0.65 |
| Assembly labor | $4.80 | $5.20 | +$0.40 |
| BMS + wiring harness | $3.50 | $3.50 | $0.00 |
| Tooling amortization | $1.20 | $1.40 | +$0.20 |
| Compliance + PPAP | $0.40 | $0.60 | +$0.20 |
| Total unit cost | $24.10 | $25.55 | +$1.45 |
The 6% dual-source cost premium is the price of risk insurance at the engineering layer. For a $25 wholesale price, this is a 5.8% margin hit — material, but absorbable.
11. Engineering KPIs: The Factory Risk Dashboard
The factory’s engineering risk dashboard should compress into six KPIs:
| KPI | Target | Trigger Threshold |
|---|---|---|
| Graphene fabric lot acceptance rate | ≥96% | <92% |
| 21700 cell vendor diversification | 2 vendors active | 1 vendor only |
| BMS firmware version drift | 0 across batch | >1 version in batch |
| PPAP submission on time | 100% | <90% |
| Field failure PPM | <2500 | >3500 |
| Tooling cycle counter logged | 100% | <95% |
The dashboard is reviewed weekly by the engineering manager and monthly by the factory GM.
12. The 21700 Cell Allocation Risk: An Engineering View
The cell allocation squeeze that has gripped the 21700 market since Q1 2026 is primarily a buyer-side concern (capacity allocation between competing programs). The engineering-side concern is different: when a buyer switches cell vendors mid-program, the BMS firmware must be re-validated against the new cell’s internal resistance profile.
The engineering supplier risk 2026 protocol for cell vendor switches:
1. Pre-switch sample run — 50-cell sample test with full charge-discharge cycle characterization.
2. BMS firmware re-validation — 2-week bench test with the new cell, validated against the original firmware hash.
3. Field pilot — 500 units with the new cell + new firmware hash, tracked for 90 days.
4. PPAP refresh — full PPAP submission with the new cell lot.
A cell vendor switch that skips the 2-week BMS re-validation typically surfaces as a 6-8% field failure rate by month 12, when the BMS terminates charge prematurely due to the cell’s slightly different voltage curve.
13. Communication Protocol With the Backup Factory’s Engineering Team
The engineering team’s relationship with the backup factory’s engineering team follows a different cadence than the buyer’s:
- Weekly — production slot booking, material lot acceptance, cell lot acceptance
- Bi-weekly — PPAP status, firmware hash reconciliation, field failure log review
- Monthly — Cpk study, mold cycle counter, tooling wear report
- Quarterly — engineering audit visit (full-day factory walkthrough)
The bi-weekly PPAP status is the most critical. A backup factory that misses two consecutive PPAP submissions is showing the early signs of a capacity or capability crisis, and the engineering team must escalate to the buyer’s sourcing desk.
14. Cost-Benefit Summary: The 2026 Engineering ROI
The fully-loaded engineering dual-source program costs:
- Material lot acceptance testing: 0.4% of revenue
- PPAP + firmware validation: 0.3% of revenue
- Backup factory tooling amortization: 0.2% of revenue
- Field failure tracking system: 0.1% of revenue
- Total program cost: ~1.0% of revenue
The benefit, sized against the avoided field failure cost:
- Field failure cost avoidance: 1.8% of revenue (one mid-size recall avoided per 18 months)
- Tariff + freight + tooling disruption avoided: 2.4% of revenue
- Total program benefit: ~4.2% of revenue
Net ROI: 4.2x annual return on the engineering dual-source program.
Conclusion
The engineering supplier risk 2026 program is the factory’s complement to the buyer’s tariff-hedge program. The two playbooks must be designed together, because the factory’s engineering risks (lot consistency, firmware drift, mold wear, IP leakage) are the upstream causes of the buyer’s downstream failures (late delivery, field returns, compliance penalty). A dual-source program that addresses only the buyer’s risks will fail the moment a fabric lot drifts 8% in resistivity or a cell vendor ships a firmware revision that breaks BMS continuity. The brands and factories that survive 2026 will be the ones that engineer both playbooks simultaneously.
Internal link: explore our [Battery Heated Apparel Factory hub for the full 2026 dual-source engineering series.]
Internal link: see [OEM ODM Manufacturing for tooling ownership, NNN stack, and brand transfer protocols.]
B2B Soft Plant #1: For OEM-ODM buyers evaluating dual-source graphene fabric programs, our engineering team can run a 3-day lot acceptance audit at our Dongguan pilot line, including sheet-resistivity bench test, wash-cycle retention, and BMS firmware hash validation.
B2B Soft Plant #2: If your program requires a 21700 cell vendor switch mid-cycle, our firmware re-validation lab can compress the 2-week bench test into 7 days for established SKU profiles.
B2B Soft Plant #3: For brands that need a written dual-source engineering playbook customized to their SKU mix, our technical-writing team can deliver a 60-page program manual in 15 business days.
Frequently Asked Questions
1. What is the minimum lot size for dual-source graphene fabric qualification? — 200 meters per lot, 3 lots minimum, with 14-day wash-cycle retention test on lot 1.
2. How long does a 21700 cell vendor switch take with full BMS re-validation? — 2 weeks bench test + 90 days field pilot = 14-16 weeks total.
3. Can a backup factory use a different BMS firmware hash than the primary? — Yes, but only after a 2-week firmware re-validation against the same cell lot.
4. What is the typical Cpk target for heated apparel production? — Cpk ≥1.33 on the 14 critical-to-quality dimensions, with Cpk ≥1.67 preferred for thermal output.
5. How is the NNN agreement stack enforced in PRC courts? — Through notarized signing + commercial court filing; enforceability is strong for documented cases.
6. What is the most common engineering-side dual-source failure? — Fabric lot resistivity drift causing thermal output mismatch between primary and backup batches.
7. How do you handle mold ownership disputes in a factory disruption? — Written tooling ownership annex, notarized, with a third-party tool-shop escrow for the hot-spare mold.
8. What is the cost premium for an engineering-grade dual-source program? — Typically 5-8% of unit cost, depending on SKU complexity and BOM lot sensitivity.
9. Does the backup factory need to be RWS certified? — Only for EU SKUs requiring the RWS claim; for US-bound SKUs, RWS is not required but recommended.
10. How is field failure data shared between primary and backup factories? — Through a shared field-failure log updated bi-weekly, with both factories reviewing the same data.
11. What is the most over-rated engineering-supplier risk in 2026? — Tooling wear. Most OEM-ODM factories track mold cycle counts correctly; the under-rated risk is firmware version drift.
12. What is the single best leading indicator of a backup factory’s health? — PPAP submission timeliness. A factory that misses two consecutive PPAP submissions is showing the early signs of a crisis.
Glossary of Terms
| Term | Definition |
|---|---|
| BMS | Battery Management System — embedded electronics managing lithium pack charge/discharge |
| BSCI | Business Social Compliance Initiative |
| CE-EMC | European Conformity – Electromagnetic Compatibility |
| Cpk | Process Capability Index |
| Dongguan | Major OEM-ODM hub in Guangdong Province, China |
| FCC Part 15B | US Federal Communications Commission unintentional radiator standard |
| Firmware hash | Cryptographic identifier for a specific firmware version |
| IEC 62133 | International safety standard for portable lithium batteries |
| IP67 | Ingress Protection rating (dust-tight, water-submersible to 1m) |
| ISO 9001 | International quality management standard |
| ISO 14001 | International environmental management standard |
| MSDS | Material Safety Data Sheet |
| NNN | Non-Disclosure, Non-Use, Non-Circumvention agreement |
| OEKO-TEX 100 | Textile safety standard for harmful substances |
| OEM-ODM | Original Equipment Manufacturer – Original Design Manufacturer |
| PPAP | Production Part Approval Process |
| REACH SVHC | EU REACH regulation’s Substances of Very High Concern |
| RoHS | Restriction of Hazardous Substances (EU) |
| RWS | Responsible Wool Standard |
| SMETA | Sedex Members Ethical Trade Audit |
| UN3481 | UN classification for lithium battery dangerous goods |
Leave a Reply