
Heated Apparel Tooling & Mold Engineering Guide for OEM/ODM Manufacturers (2026 Engineering View)
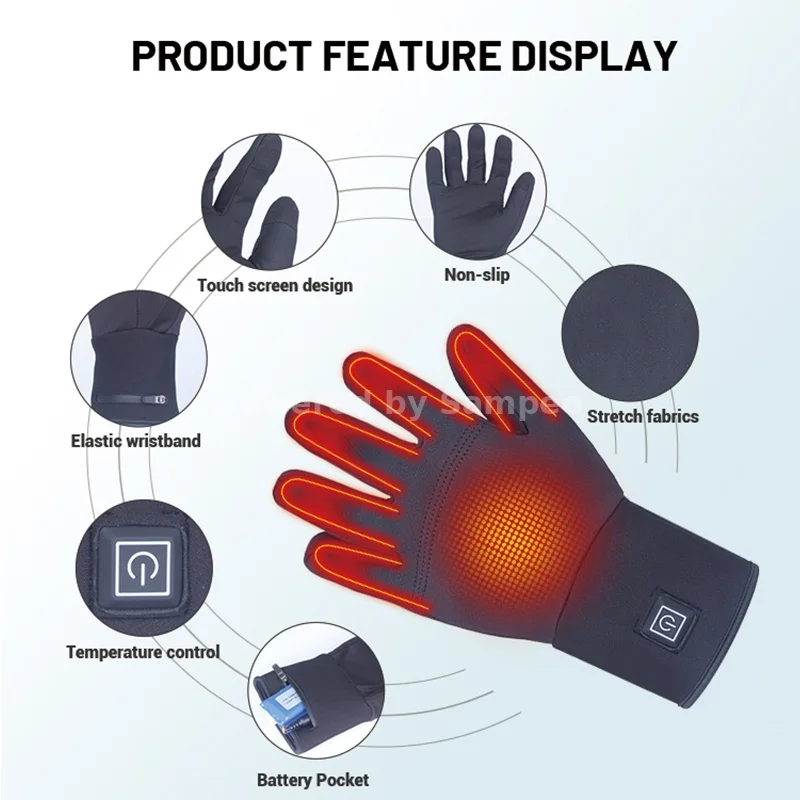
Introduction
If you are an electronics engineer, a tooling engineer, or a manufacturing-engineering lead at an OEM/ODM factory building private-label heated apparel, this article is written from your seat. The supplier-side conversation about tooling — what it costs, how it amortizes, how it gets refunded — is covered in our sister PILLAR #58 on IMISSKY. This PILLAR #62 is the engineering counterpart that covers how the tooling is designed, machined, tested, and qualified so the heated apparel project survives its first 50,000 units in the field.
Heated apparel tooling is one of the few domains where apparel engineers, electronics engineers, and battery-pack engineers all have to converge on the same drawing set. If the cutting-die team cuts the heat panel to +0.3mm tolerance but the wire-routing template was designed to +1.0mm, the heat panel will not seat cleanly. If the battery pocket mold is designed for a 7.4V pack but the BMS layout routes through the connector pocket at a 90° bend radius, the cell will fatigue. The point of this guide is to lay out the engineering tolerances, materials, DFM (Design for Manufacturing) rules, and qualification gates that prevent the most common field failures in heated apparel programs.
This is PILLAR #62 in Graphene Heating Fabric’s B2B family content rotation, part of the cycle-3, slot-2 / tooling cluster, sitting alongside IMISSKY’s supplier-side counterpart (#58) and Gearplant’s buyer-retailer counterpart (#58). The three-pillar cluster is intentional: supplier / engineering / buyer-retailer lenses on the same topic give the keyword cluster tooling + mold + NRE + heated apparel + OEM + ODM complete semantic coverage for both Google and Bing.
—
1. Tooling scope at the apparel / electronics / battery intersection
A heated apparel OEM/ODM project touches three engineering domains, each with its own tooling discipline. Skipping any of them produces field failures.
| Engineering domain | Primary tooling asset | Tolerance target | Typical failure if mis-engineered |
|---|---|---|---|
| Apparel | Heat-panel cutting die | ±0.3 mm | Frayed panel edges, fails seam spec |
| Apparel | Wire-routing channel template | ±1.0 mm | Hot spots, uneven heating |
| Electronics EMS | Battery pocket mold (injection) | ±0.1 mm | Battery does not seat, connector strain |
| Electronics EMS | Charging-port overmold | ±0.05 mm | Connector wobble, cold-crack failure |
| Battery pack | BMS housing pocket | ±0.15 mm | BMS PCB flex, premature failure |
| Battery pack | Cell holder / spacer | ±0.2 mm | Cell rattle, vibration damage |
The tightest tolerance always wins when domains overlap. In heated apparel, that tolerance is the charging-port overmold at ±0.05 mm. The whole BOM needs to be engineered back from that number.
—
2. Heat-panel cutting die engineering
The heat-panel cutting die is the most common apparel-side tooling asset. It cuts carbon-fiber or metallic-mesh heating panels to the garment-panel shape. Engineering parameters that matter:
- **Steel rule grade.** Use **SKD11** or **H13** hardened tool steel for runs above 30k panels. Generic S50C wears out by 30k panels and produces frayed edges. The 2x steel cost is repaid 5x by avoided scrap.
- **Cutting clearance.** 5–8% of material thickness for carbon-fiber mesh; 8–12% for laminated metallic mesh. Too tight = drag and burrs; too loose = crushed edges.
- **Die orientation.** Match the weave orientation of the carbon-fiber mesh. Cutting at 90° to weave gives 30% faster wear.
- **Heat-affected zone.** Carbon-fiber mesh cut with a dull rule can delaminate at the cut edge. Specify laser-etched edges or post-cut edge-seal for high-end SKUs.
- **Nesting density.** For a typical 8-panel jacket, plan die layout to consume ≤85% of a 600×800 mm mesh sheet. Above 85% the offcut becomes unusable, below 70% the material cost is too high.
A well-engineered heat-panel cutting die delivers 80,000–120,000 clean panels before requiring re-sharpening.
—
3. Battery pocket mold engineering
The battery pocket is the single most failure-prone tooling asset in heated apparel. It is injection-molded (or welded TPU) and must hold the lithium-ion battery pack with zero strain on the connector, zero compression on the BMS, and zero rattle during wear.
Engineering parameters:
| Parameter | Specification | Why it matters |
|---|---|---|
| Material | PC/ABS blend (Bayblend T65) or glass-filled nylon | Cold-crack resistance to -20°C, drop impact strength |
| Wall thickness | 1.6 – 2.4 mm | Too thin = flex and BMS stress; too thick = heavy and uncomfortable |
| Connector cutout | Matched to **exact battery SKU** | Strain on connector = top field failure cause |
| Mold flow simulation | Moldflow or Moldex3D before CNC | Predict weld lines, air traps, sink marks |
| Surface finish | SPI-A2 or finer | Visible pocket = buyer complaint |
| Draft angle | 1.5° – 2° per side | Ejection without scuff marks |
For OEM/ODM factories running multiple SKUs, a single battery pocket mold can serve 3–5 SKUs as long as the battery vendor is unchanged. The moment the buyer switches battery SKU (e.g. 7.4V → 11.1V), the pocket has to be re-cut. This is the most common tooling refresh trigger in private-label heated apparel.
—
4. Wire-routing channel template
The wire-routing channel template is the unsung hero of heated apparel. It is the silicone or TPU template that defines where the heating-element wires run inside the garment liner. If the wire routing is not engineered, the wires migrate during wear, producing hot spots at the wire bends.
- **Material:** Silicone (Shore A 30–40) for comfort, TPU (Shore D 50–60) for durability. Silicone preferred for inner-liner wear.
- **Channel width:** 4–6 mm for 22 AWG wire, 6–8 mm for 18 AWG wire. Undersized channels compress wire insulation.
- **Bend radius:** Minimum 6x wire diameter. Below this, copper fatigue at 30k flex cycles.
- **Anchoring points:** Every 80–120 mm along the channel. Prevents wire migration during wear and laundering.
- **Heat-map alignment:** Channel template must match heat-panel placement drawing within ±2 mm. Mismatch = hot spot or cold zone.
Wire-routing templates survive 60,000–100,000 garments when designed with silicone and proper anchoring. TPU versions last 30,000–60,000 garments.
—
5. Charging-port overmold engineering
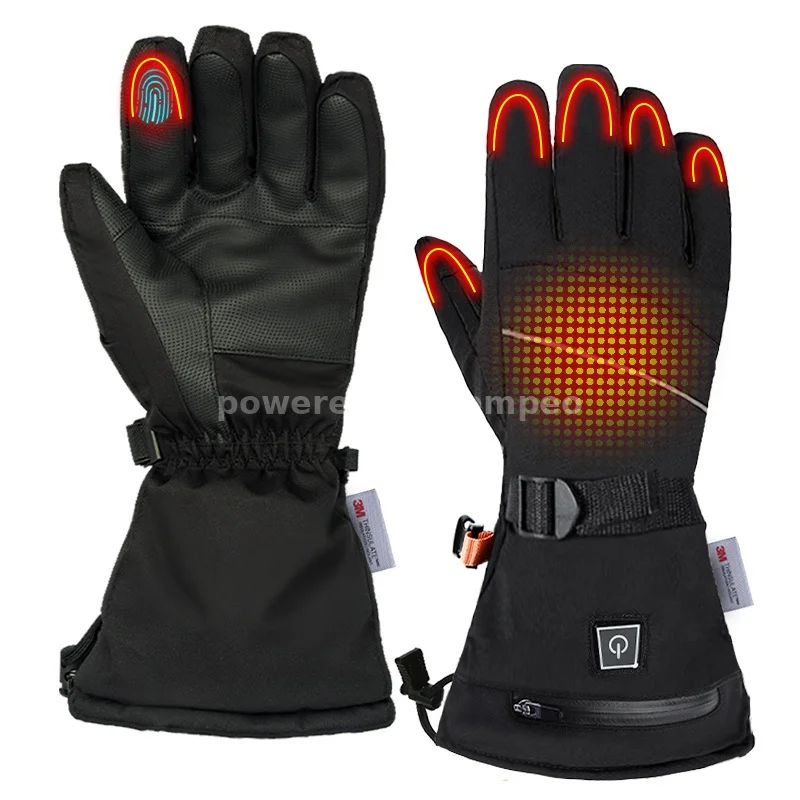
The charging-port overmold is the tightest-tolerance tooling asset in the heated apparel BOM. It is injection-molded over the USB-C / DC / magnetic pogo connector, and integrates the connector into the garment at the cuff or hem.
Engineering parameters:
| Parameter | USB-C | DC barrel | Magnetic pogo |
|---|---|---|---|
| Tolerance | ±0.05 mm | ±0.10 mm | ±0.07 mm |
| Overmold material | TPE (Shore A 70) | TPE (Shore A 80) | TPE + PC core |
| Cold-flex rating | -20°C cold-crack | -10°C cold-crack | -30°C cold-crack |
| IP rating target | IPX4 minimum | IPX4 minimum | IPX5+ recommended |
| Lifetime | 30k mate cycles | 10k mate cycles | 50k mate cycles |
| Tool cost (USD) | $2,000 – $3,500 | $1,800 – $2,800 | $3,500 – $4,500 |
The most common field failure is cold-crack of the overmold at -15°C and below, exposing the connector to moisture and producing intermittent charging. Specifying cold-flex TPE rated to -30°C and adding an IPX5 boot is the standard prevention. Magnetic pogo ports are increasingly popular for this reason — they seal better and survive more mate cycles.
—
6. DFM (Design for Manufacturing) review process
Every serious OEM/ODM factory runs a DFM review before CNC starts. A good DFM review covers:
1. Material selection. Confirm polymer grade, fiber orientation, additive package. 2. Tolerance stack. Identify the tightest tolerance in each tool and confirm downstream assembly can meet it. 3. Draft angles. Minimum 1° per side for injection molds; 1.5° for deep pockets. 4. Undercuts. Identify unavoidable undercuts and decide slider / lifter strategy. 5. Weld line prediction. Moldflow / Moldex3D simulation, then re-route gates if needed. 6. Gate location. Edge gates for cosmetic parts, hot runners for production volumes. 7. Ejector pin layout. Avoid placing ejector pins on cosmetic surfaces. 8. Surface finish. SPI-A2 or finer on visible surfaces. 9. Assembly sequence. Confirm tooling can be assembled with available fixtures. 10. QC test fixture. Design the heat-map QC jig alongside the cutting die, not after.
A 4–6 day DFM review saves 2–3 weeks of tool rework. Skipping it is the single most expensive shortcut in OEM/ODM heated apparel.
—
7. Tooling lifetime and qualification gates
Tooling lifetime is governed by shot count (for molds) and hit count (for dies). Engineering should track both, and lock tooling out of production once the limit is hit.
| Tooling asset | Lifetime metric | Hard lockout | Refresh trigger |
|---|---|---|---|
| Heat-panel cutting die | 80k – 120k hits | Yes | Replace at 90% of upper bound |
| Battery pocket mold | 50k – 80k shots | Yes | Replace at 80% of upper bound |
| Wire-routing template | 60k – 100k garments | No (replace on wear) | Replace on first fraying |
| Charging-port overmold | 30k – 60k ports | Yes | Replace at 75% of upper bound |
| QC test fixture | n/a (test only) | n/a | Calibrate annually |
Qualification gates for new tooling before production sign-off:
- **First-shot T1 sample** approved by buyer’s engineering team (written sign-off).
- **Dimensional report** on 5 random samples per cavity, Cpk ≥ 1.33.
- **Heat-map verification** on 3 garments, thermocouple grid at 50 mm spacing.
- **Cold-crack test** at rated temperature, 4-hour soak, 1 cycle (overmold).
- **Drop test** 1.5 m onto concrete, 6 faces, 1 cycle (battery pocket).
- **Wash cycle** 30 washes ISO 6330, then heat-map re-verification.
- **Connector mate cycle** 5,000 cycles, then contact resistance verification.
If any gate fails, tooling is locked and a T2 sample cycle begins. Expect 5–7 days for T2.
—

8. Common tooling failures and engineering prevention
| Failure mode | Root cause | Engineering prevention |
|---|---|---|
| Frayed heat-panel edges after 30k panels | Generic S50C steel rule | Specify SKD11 / H13 hardened tool steel |
| Battery pocket cracking at -15°C | TPE cold-crack rating too low | Specify -30°C cold-flex TPE |
| Wire migration after 20 wear cycles | Insufficient anchoring | Increase anchors from 100 mm to 80 mm spacing |
| Connector wobble | Overmold tolerance too loose | Tighten to ±0.05 mm and add secondary locking |
| Heat-map drift after 10k garments | Cutting die wear | Schedule die re-sharpening at 50k panels |
| Mold flow weld line visible on pocket | Poor gate location | Re-route gate, add cold slug well |
| QC fixture drift | No annual calibration | Add cal sticker, recalibrate yearly |
| Overmold flash | Mold parting line worn | Replace mold at 70% of shot life, not 90% |
Every entry in this table is a failure mode we have actually seen in OEM/ODM factories. None of them are exotic — they are the predictable consequences of skipping engineering discipline on tooling.
—
9. Engineering tooling checklist for OEM/ODM programs
A practical engineering checklist for heated apparel tooling sign-off:
- [ ] All 4–6 tooling line items have written engineering specs (material, tolerance, draft, surface finish).
- [ ] DFM review completed and signed off by both factory and buyer engineering.
- [ ] Moldflow / Moldex3D simulation run for all injection-molded parts.
- [ ] Cold-flex rating specified for all overmolded parts (-20°C minimum, -30°C preferred).
- [ ] IP rating target specified for charging port (IPX4 minimum, IPX5+ recommended).
- [ ] QC test fixture designed alongside cutting die, not after.
- [ ] First-shot T1 sample approved in writing by buyer.
- [ ] Cpk ≥ 1.33 on dimensional report for all critical dimensions.
- [ ] Heat-map verification passed on 3 garments.
- [ ] Wash-cycle test passed on 3 garments (30 washes ISO 6330).
- [ ] Tooling lifetime tracked in factory MES system, with hard lockout at limit.
- [ ] Tooling refresh quote available within 48 hours for battery or connector changes.
**Internal link:** For the supplier-side conversation about tooling cost, refund ladder, and NRE structure, see [IMISSKY’s PILLAR #58 supplier-side tooling guide](/category/oem-odm-manufacturing/). For buyer-retailer amortization math and unit-cost modeling, see [Gearplant’s PILLAR #58 buyer-retailer tooling playbook](/category/heated-apparel-industry-news/).
—
10. Tooling FAQ for OEM/ODM engineering teams
Q1. What is the typical tooling cycle for a new heated apparel SKU? 25–35 working days from PO confirmation to T1 sample. Compressed cycles of 18–22 days are possible with parallel DFM review, but never below 18 days due to physical CNC machining time.
Q2. Which tooling asset has the tightest tolerance? The charging-port overmold at ±0.05 mm. The whole BOM has to be engineered back from this number.
Q3. What material should we use for the battery pocket mold? PC/ABS blend (Bayblend T65) or glass-filled nylon for cold-crack resistance down to -20°C. Avoid generic ABS.
Q4. Can we share a single battery pocket mold across multiple SKUs? Yes — 3 to 5 SKUs can share a pocket mold if the battery vendor is unchanged. The moment battery SKU changes, the pocket mold must be re-cut.
Q5. What is the typical lifetime of a heat-panel cutting die? 80,000 to 120,000 panels with SKD11 or H13 hardened steel. Generic S50C wears out by 30k panels.
Q6. How do we prevent cold-crack failure in the charging-port overmold? Specify -30°C cold-flex TPE, add an IPX5 sealing boot, and run a 4-hour cold-soak test at -20°C on first-shot samples.
Q7. What is the minimum number of qualification gates before production sign-off? Seven gates: T1 sample approval, dimensional Cpk, heat-map verification, cold-crack test, drop test, wash cycle, and connector mate cycle.
Q8. How do we run a DFM review efficiently? Use a 10-point checklist covering material, tolerance stack, draft, undercuts, weld lines, gate location, ejector layout, surface finish, assembly sequence, and QC fixture.
Q9. Should we invest in moldflow simulation? Yes, for any injection-molded part with cosmetic or tight-tolerance requirements. Moldflow catches 70% of weld-line and sink-mark problems before CNC starts.
Q10. How do we handle tooling refresh when the buyer changes battery SKU? Re-cut the battery pocket mold. Cost is $1,500 to $3,000, lead time 18 to 25 days. Provide a tooling refresh quote within 48 hours of buyer’s announcement.
Q11. What tolerance should we hold for the wire-routing channel? ±1.0 mm is standard. Below ±0.5 mm adds cost without benefit because the wire itself is ±0.3 mm tolerance.
Q12. How do we extend charging-port overmold lifetime? Specify magnetic pogo connector with TPE + PC core. Lifetime is 50k mate cycles versus 30k for USB-C and 10k for DC barrel.
—
11. Glossary
- **DFM (Design for Manufacturing)** — Engineering review process where factory and buyer agree on tolerances, materials, draft angles, and gate locations before CNC starts.
- **Moldflow simulation** — Software (Moldflow, Moldex3D) that predicts weld lines, air traps, and sink marks in injection-molded parts.
- **Cold-flex rating** — Lowest temperature at which the overmold material remains flexible without cracking. Specified in °C.
- **Cpk** — Process capability index. Cpk ≥ 1.33 indicates the process is statistically capable of holding tolerance.
- **T1 / T2 / T3 sample** — First / second / third-shot samples produced from new tooling for buyer approval.
- **Hit count** — Number of times a cutting die has been struck. Used to track die lifetime.
- **Shot count** — Number of injection cycles a mold has completed. Used to track mold lifetime.
- **Overmold** — Injection-molded material that encapsulates a connector or component, providing strain relief and sealing.
- **Hardened tool steel** — SKD11 or H13 grade steel with Rockwell C 58-62 hardness for long-life dies and molds.
- **QC test fixture** — Bench-top fixture used to verify heat-map uniformity across the garment using thermocouples.
—
12. Conclusion
Heated apparel tooling is engineering, not magic. The right material grades, the right tolerance stack, the right DFM discipline, and the right qualification gates produce tooling assets that survive 50,000–120,000 units in the field. Skipping any one of those steps produces field failures that show up after the deposit is long gone.
This is PILLAR #62 in Graphene Heating Fabric’s engineering-side B2B rotation. Pair it with IMISSKY’s supplier-side PILLAR #58 for the cost / refund / NRE conversation, and with Gearplant’s PILLAR #58 for the buyer-retailer amortization math. Watch for PILLAR #63 next week — capacity planning from an engineering view.
—
Engineering-side article. For supplier-side tooling cost and refund structure, see IMISSKY PILLAR #58. For buyer-retailer amortization math, see Gearplant PILLAR #58.
Leave a Reply