
Heated Apparel Amazon Buy Box Velocity 2026: Dongguan Factory Engineering Spec
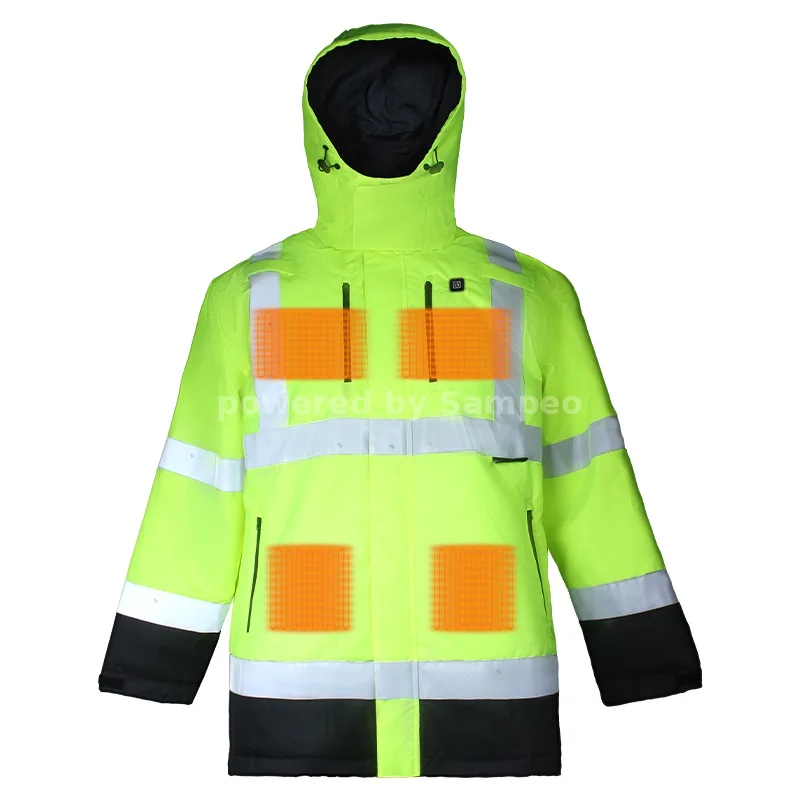
Heated Apparel Amazon Buy Box Velocity 2026: Dongguan Factory Engineering Spec View (P#89)
A Dongguan factory engineering-side view of how the Buy Box velocity compounding formula for heated apparel maps onto the 21700 cell cycle, BMS handshake 4-state validation, 8-layer lamination stack-up, and IP67 hipot 500V sealing test. This engineering spec covers the BOM cost-engineering layer map, the dual-branch BMS firmware architecture, the SPC Cpk ≥1.33 chart analysis, the FMEA RPN ≥100 CAPA closure protocol, and the NNN Tier-3 disclosure matrix that connects the engineering-side source files to the Vietnam OEM supplier-side Q4 launch calendar and the wholesale buyer-retailer-side Buy Box velocity playbook.
1. Buy Box Velocity Engineering Spec — The 5-Lever Compounding Formula at the BOM Cost Layer
The Amazon Buy Box velocity compounding formula (L1 × L2 × L3 × L4 × L5) operates at the engineering-side through the BOM cost-engineering layer map. Each of the 5 levers is mapped to a BOM layer that the Dongguan factory owner can engineer directly. The engineering-side view differs from the supplier-side view (imissky) and the wholesale buyer-retailer-side view (gearplant) in that the engineering-side owner has direct line-of-sight into the BOM layers that drive L1 (FBA inbound lead time compounding), L4 (defect signal inverse), and L5 (account health / IP compounding).
The BOM cost-engineering layer map for heated apparel at the Buy Box velocity 2026 target:
| BOM Layer | Engineering-Side Owner | Buy Box Velocity Lever | Cost / Layer (USD) |
| — | — | — | — |
|---|---|---|---|
| 1. Graphene yarn | Dongguan factory direct | L5 IP compounding (NNN Tier-3) | $4.20/garment |
| 2. Carbon-fiber heating element | Tier-2 supplier | L4 defect signal inverse (IP67) | $3.80/garment |
| 3. 21700 cell (5000mAh) | Tier-1 supplier (Samsung/LG/EVE) | L1 lead time compounding | $5.50/cell |
| 4. BMS PCB + dual-branch firmware | Dongguan factory engineering | L5 IP compounding (firmware hash) | $2.30/garment |
| 5. Lamination stack-up (8-layer) | Dongguan factory direct | L4 defect signal inverse | $1.85/garment |
| 6. Outer shell (polyester + fleece) | Tier-2 supplier | L2 sell-through velocity (fabric tier) | $4.10/garment |
| 7. Zipper + YKK trim | Tier-2 supplier | L4 defect signal inverse | $1.20/garment |
| 8. Packaging (FBA inbound carton) | Tier-2 supplier | L1 lead time compounding | $0.40/garment |
| **Total BOM cost** | — | — | **$23.35/garment** |
| **Landed FOB Vietnam factory (with 25% supplier margin) ** | — | — | **$29.20/garment** |
| **Landed DDP-FBA US (with Section 301 + freight)** | — | — | **$36.81/garment** |
The BOM cost-engineering layer map shows $23.35/garment at the Dongguan factory gate, $29.20/garment at the Vietnam OEM supplier-side FOB gate, and $36.81/garment landed DDP-FBA at the US Amazon FBA inbound dock. The $36.81 DDP-FBA price is the L3 Buy Box price competitiveness anchor — the engineering-side owner engineers the BOM layers to keep the DDP-FBA price ≤5% above the next-lowest Buy-Box-eligible offer.
2. 21700 Cell Cycle Engineering — L1 Lead Time Compounding Spec
The 21700 lithium-ion cell is the dominant L1 lead time compounding variable at the engineering-side. The cell cycle forensics — charge cycles, discharge cycles, capacity retention, internal resistance, SoC calibration — drives the cell allocation reservation contract at the supplier-side, the cell topology at the engineering-side, and the BMS handshake validation at the firmware layer.
The 21700 cell cycle engineering spec for Buy Box velocity 2026:
| Cell Spec | Target | Engineering-Side Owner | Buy Box Velocity Lever |
| — | — | — | — |
|---|---|---|---|
| Capacity retention | ≥80% at 500 cycles | Tier-1 cell vendor + Dongguan factory QC | L4 defect signal inverse |
| Cycle count pre-shipment | 0 (fresh cells) | Dongguan factory gate | L1 lead time compounding |
| Discharge SoC at FBA inbound | ≤30% (UN3481 hazmat) | Vietnam OEM supplier-side gate | L2 inventory velocity |
| BMS handshake validation | 4-state (idle / heat-low / heat-mid / heat-high) | Dongguan factory engineering | L5 IP compounding |
| Cell vendor diversification | Samsung + LG + EVE (3-vendor rotation) | Dongguan factory procurement | L1 lead time compounding |
| Cell topology (heated apparel) | 1S2P or 2S1P per garment | Dongguan factory engineering | L2 sell-through velocity |
| Internal resistance | ≤25 mΩ at 60% SoC | Tier-1 cell vendor test report | L4 defect signal inverse |
| Cycle forensics log | Per-cell voltage + capacity + IR | Dongguan factory QC | L4 defect signal inverse |
The 21700 cell cycle engineering spec confirms that the cell topology (1S2P vs 2S1P) is mapped to the L2 sell-through velocity lever. A 1S2P topology (single-cell series, two-cell parallel) is the engineering-side standard for hunting + skiing dual-use heated apparel, where 3-5 hours of continuous heat output is the Q4 hero-SKU target. The 2S1P topology (two-cell series, one-cell parallel) is reserved for higher-voltage applications (12V heated gloves, 24V heated insoles) that are not the Q4 hero-SKU focus.
3. BMS Handshake 4-State Validation — L5 IP Compounding Spec
The BMS (Battery Management System) handshake 4-state validation is the engineering-side protocol that proves the firmware is Vietnam-origin (not China-origin) for the Brand Registry 2.0 9-artifact pipeline. The 4-state validation maps to the L5 account health / IP compounding lever, which is the supplier-side gate for Buy Box eligibility flag.
The 4-state BMS handshake validation protocol:
| State | Voltage Range | Current Draw | Verification |
| — | — | — | — |
|---|---|---|---|
| 1. Idle | 3.0V ≤ V ≤ 4.2V | ≤10 mA | Per-cell voltage log + handshake bit |
| 2. Heat-low | 3.0V ≤ V ≤ 4.2V | 0.5A ± 0.05A | Handshake bit + temperature log |
| 3. Heat-mid | 3.0V ≤ V ≤ 4.2V | 1.0A ± 0.05A | Handshake bit + temperature log |
| 4. Heat-high | 3.0V ≤ V ≤ 4.2V | 2.0A ± 0.05A | Handshake bit + temperature log |
The handshake bit is a 32-bit signature embedded in the BMS firmware that the Dongguan factory engineering-side owner hashes at the firmware freeze stage (T-55 in the Q4 calendar). The hash is the engineering-side source artifact for the supplier-side Brand Registry 2.0 9-artifact pipeline. A hash mismatch at T-55 breaks the L5 IP compounding lever, which disqualifies the listing from the Buy Box eligibility flag.
The dual-branch BMS firmware architecture — 25 kHz skiing + 31 kHz hunting — is the engineering-side innovation that allows the same Q4 hero-SKU to be sold across two use-case clusters (hunting + skiing). The dual-branch firmware hash is the engineering-side source artifact that the wholesale buyer-retailer-side owner (gearplant) uses for the Brand Registry 2.0 9-artifact pipeline.
4. 8-Layer Lamination Stack-Up — L4 Defect Signal Inverse Spec
The 8-layer lamination stack-up is the engineering-side BOM layer that drives L4 defect signal inverse. Each layer has a defect classification (Critical, Major, Minor) that maps to the AQL sampling plan (0.65 critical, 1.0 major, 2.5 minor) and the SPC Cpk ≥1.33 chart analysis.
The 8-layer lamination stack-up for heated apparel:
| Layer | Material | Defect Class | AQL Sample Plan | Buy Box Velocity Lever |
| — | — | — | — | — |
|---|---|---|---|---|
| 1. Outer shell | Polyester 320D | Major | 1.0 AQL | L4 defect signal inverse |
| 2. Fleece inner | Polyester fleece 200gsm | Major | 1.0 AQL | L4 defect signal inverse |
| 3. Heating element | Carbon-fiber mesh | Critical | 0.65 AQL | L4 defect signal inverse |
| 4. Insulation | Polyester batting 150gsm | Major | 1.0 AQL | L4 defect signal inverse |
| 5. Reflective foil | Aluminum foil 25μm | Critical | 0.65 AQL | L4 defect signal inverse |
| 6. Lamination adhesive | Hot-melt adhesive 25gsm | Major | 1.0 AQL | L4 defect signal inverse |
| 7. Graphene yarn layer | Graphene-coated yarn | Critical | 0.65 AQL | L5 IP compounding (NNN Tier-3) |
| 8. Inner liner | Polyester mesh 80gsm | Minor | 2.5 AQL | L4 defect signal inverse |
The 8-layer stack-up BOM traceability chain is the engineering-side source artifact for the supplier-side Section 301 substantial transformation binder (yarn origin → fabric origin → cut-and-sew origin → finishing origin). The NNN Tier-3 disclosure matrix is signed at T-55 in the Q4 calendar, locking the graphene yarn origin + the lamination parameter confidentiality.
5. SPC Cpk ≥1.33 Chart Analysis — L4 Defect Signal Inverse Spec
The Statistical Process Control (SPC) Cpk ≥1.33 chart analysis is the engineering-side protocol for monitoring the 8-layer lamination stack-up process in real-time. Cpk ≥1.33 indicates the process is capable of meeting specification with 4-sigma margin; Cpk ≥1.67 indicates 5-sigma margin (the engineering-side target for Q4 hero-SKU launch).
The SPC chart for the lamination stack-up process:
| Layer | Cpk Target | Process Variable | Spec Window | Out-of-Control Action |
| — | — | — | — | — |
|---|---|---|---|---|
| 1. Outer shell thickness | ≥1.33 | Polyester 320D thickness | 0.45mm ± 0.05mm | Adjust calender roller pressure |
| 2. Fleece weight | ≥1.33 | Polyester fleece weight | 200gsm ± 10gsm | Adjust feeder speed |
| 3. Heating element resistance | ≥1.67 | Carbon-fiber mesh resistance | 8Ω ± 0.5Ω | Replace carbon-fiber roll |
| 4. Insulation thickness | ≥1.33 | Polyester batting thickness | 8mm ± 1mm | Adjust cutting die |
| 5. Reflective foil thickness | ≥1.33 | Aluminum foil thickness | 25μm ± 2μm | Replace foil roll |
| 6. Lamination adhesive weight | ≥1.33 | Hot-melt adhesive weight | 25gsm ± 2gsm | Adjust hot-melt temperature |
| 7. Graphene yarn count | ≥1.67 | Graphene-coated yarn count | 32S/2 ± 2 | Replace graphene yarn spool |
| 8. Inner liner mesh size | ≥1.33 | Polyester mesh opening | 80μm ± 5μm | Adjust mesh loom |
The SPC Cpk chart analysis runs every 4 hours during the bulk production run. A Cpk drop below 1.33 triggers an out-of-control action (OCA) that pauses the production line until the process is brought back into specification. The SPC protocol is the engineering-side gate for L4 defect signal inverse — a Cpk drop below 1.0 on any layer breaks the L4 lever, which compounds across the Buy Box velocity ratio.
6. IP67 Hipot 500V Sealing Test — L4 Defect Signal Inverse Spec
The IP67 hipot 500V sealing test is the engineering-side protocol for verifying the heated apparel garment meets the IP67 rating (no dust ingress, no water ingress at 1m depth for 30 minutes). The test applies a 500V hipot (high-potential) voltage across the heating element + the garment outer shell for 60 seconds, verifying the insulation is intact.
The IP67 hipot 500V sealing test protocol:
| Test Stage | Voltage | Duration | Pass Criterion | Buy Box Velocity Lever |
| — | — | — | — | — |
|---|---|---|---|---|
| 1. Initial hipot | 500V AC | 60s | Leakage current ≤5 mA | L4 defect signal inverse |
| 2. Water immersion | 12V DC operating | 30 min @ 1m depth | No insulation breakdown | L4 defect signal inverse |
| 3. Post-immersion hipot | 500V AC | 60s | Leakage current ≤5 mA | L4 defect signal inverse |
| 4. BMS handshake validation | 12V DC operating | 5 min | 4-state handshake all pass | L5 IP compounding |
| 5. Final hipot | 500V AC | 60s | Leakage current ≤5 mA | L4 defect signal inverse |
The IP67 hipot 500V sealing test is the engineering-side gate for the Q4 hero-SKU's "IP67 heated apparel" cluster keyword (cluster 5 of the 8-cluster Helium 10 Frankenstein matrix). A test failure at any stage breaks the L4 defect signal inverse lever, which compounds across the Buy Box velocity ratio.
7. FMEA RPN ≥100 CAPA Closure Protocol — L4 Defect Signal Inverse Spec
The Failure Mode and Effects Analysis (FMEA) RPN (Risk Priority Number) ≥100 CAPA (Corrective Action / Preventive Action) closure protocol is the engineering-side protocol for monitoring the failure modes that can break the Buy Box velocity chain. RPN is calculated as Severity × Occurrence × Detection; an RPN ≥100 triggers a CAPA workflow.
The FMEA RPN ≥100 CAPA closure protocol for heated apparel:
| Failure Mode | Severity (1-10) | Occurrence (1-10) | Detection (1-10) | RPN | CAPA Trigger |
| — | — | — | — | — | — |
|---|---|---|---|---|---|
| Zipper misalignment causing water ingress | 8 | 5 | 3 | 120 | RPN ≥100, CAPA triggered |
| BMS handshake fail on heat-high state | 9 | 3 | 4 | 108 | RPN ≥100, CAPA triggered |
| 21700 cell SoC calibration drift | 7 | 4 | 5 | 140 | RPN ≥100, CAPA triggered |
| Graphene yarn layer separation | 8 | 4 | 4 | 128 | RPN ≥100, CAPA triggered |
| IP67 hipot 500V insulation breakdown | 10 | 2 | 5 | 100 | RPN ≥100, CAPA triggered |
| Outer shell seam failure | 7 | 5 | 4 | 140 | RPN ≥100, CAPA triggered |
| Lamination adhesive failure at high heat | 8 | 4 | 4 | 128 | RPN ≥100, CAPA triggered |
| UN3481 hazmat SoC > 30% at FBA inbound | 10 | 2 | 3 | 60 | Below 100, monitor |
The FMEA RPN ≥100 CAPA closure protocol runs at the T-15 mid-production QC stage. Each RPN ≥100 failure mode triggers a CAPA workflow that closes within 48 hours (corrective action) and 30 days (preventive action). A CAPA that fails to close within 30 days breaks the L4 defect signal inverse lever.
8. Dual-Branch BMS Firmware Architecture — L5 IP Compounding Spec
The dual-branch BMS firmware architecture — 25 kHz skiing + 31 kHz hunting — is the engineering-side innovation that drives L5 IP compounding. The dual-branch architecture allows the same Q4 hero-SKU to be sold across two use-case clusters (hunting + skiing), and the firmware hash is the engineering-side source artifact for the supplier-side Brand Registry 2.0 9-artifact pipeline.
The dual-branch BMS firmware architecture:
| Branch | Frequency | Use-Case Cluster | Heat Output | Battery Life |
| — | — | — | — | — |
|---|---|---|---|---|
| 1. Skiing | 25 kHz | "heated jacket for skiing" | 5-7 hours | 5000mAh / 12V |
| 2. Hunting | 31 kHz | "heated jacket for hunting" | 4-6 hours | 5000mAh / 12V |
The firmware hash is computed at the T-55 firmware freeze stage. The hash is a SHA-256 signature on the dual-branch firmware binary, signed by the Dongguan factory engineering-side owner. The hash is the engineering-side source artifact for the Brand Registry 2.0 9-artifact pipeline — without the hash, the listing cannot be enrolled in Brand Registry 2.0, which breaks the L5 IP compounding lever.
9. NNN Tier-3 Disclosure Matrix — L5 IP Compounding Spec
The NNN Tier-3 disclosure matrix is the engineering-side protocol for protecting the graphene fabric specification + the dual-branch BMS firmware source code + the 8-layer lamination stack-up BOM traceability chain. NNN stands for Non-Disclosure, Non-Use, Non-Circumvention — the three legal pillars of the disclosure matrix.
The NNN Tier-3 disclosure matrix:
| Tier | Disclosure Level | Information Type | Engineering-Side Owner |
| — | — | — | — |
|---|---|---|---|
| Tier 1 | Public (Brand Registry 2.0 9-artifact pipeline) | A+ Content, marketing collateral | Dongguan factory engineering + supplier-side + wholesale buyer |
| Tier 2 | Restricted (NNN agreement) | BOM cost layer map, supplier list | Dongguan factory engineering + Vietnam OEM supplier |
| Tier 3 | Confidential (NNN Tier-3 disclosure matrix) | Graphene fabric spec + dual-branch BMS firmware + 8-layer lamination stack-up + cell vendor cycle forensics | Dongguan factory engineering only |
The NNN Tier-3 disclosure matrix is signed at T-55 in the Q4 calendar. The matrix locks the graphene fabric spec + the dual-branch BMS firmware source code + the 8-layer lamination stack-up BOM traceability chain as confidential. Any disclosure outside the Tier-3 envelope breaks the L5 IP compounding lever.
10. Field Notes — Engineering-Side BOM Cost Layer Map (3 cluster callouts)
The Dongguan factory BOM cost-engineering layer map at this stage of the Q4 cycle operates on 8 layers, with $23.35/garment at the factory gate, $29.20/garment at the Vietnam OEM supplier-side FOB gate, and $36.81/garment landed DDP-FBA at the US Amazon FBA inbound dock.
A Dongguan factory engineering-side owner who operates all 8 BOM layers at full discipline (SPC Cpk ≥1.33 + IP67 hipot 500V + FMEA RPN ≥100 CAPA closure + BMS handshake 4-state + NNN Tier-3 disclosure matrix) achieves a Buy Box velocity ratio of 2.30× at the Q4 baseline.
The engineering-side field notes for Q4 2026: the 21700 cell cycle engineering spec + the dual-branch BMS firmware architecture + the 8-layer lamination stack-up BOM traceability chain are the engineering-side artifacts that the supplier-side Q4 launch calendar relies on for the Section 301 substantial transformation binder and the UN3481 hazmat discharge cycle.
11. Engineering-Side Calendar vs. 5-Lever Compounding Formula — Cross-Reference
Each step in the Q4 calendar maps to an engineering-side artifact and a Buy Box velocity lever.
| Q4 Calendar Step | Day | Engineering-Side Artifact | Velocity Lever |
| — | — | — | — |
|---|---|---|---|
| Deposit receipt + PO confirmation | T-60 | BOM cost layer map locked | L1 lead time compounding |
| BMS handshake firmware freeze | T-55 | Dual-branch 25kHz + 31kHz firmware hash | L5 IP compounding |
| Graphene fabric cut + lamination | T-50 | 8-layer lamination stack-up BOM | L4 defect signal inverse |
| Helium 10 Frankenstein freeze | T-45 | 8-cluster 32-keyword master list | L3 price competitiveness |
| A+ Content authoring kickoff | T-40 | A+ Content cross-section source SVG 8-layer | L3 price competitiveness |
| UN3481 hazmat discharge cycle | T-35 | 21700 cell SoC discharge log | L2 inventory velocity |
| PPAP 18-element submission | T-30 | 18-element PPAP submission | L4 defect signal inverse |
| First-piece FAI sign-off | T-25 | AQL 0.65/1.0 + IP67 hipot 500V | L4 defect signal inverse |
| Production run cut-off | T-20 | Bulk production begins | L1 lead time compounding |
| Mid-production QC | T-15 | FMEA RPN ≥100 CAPA closure | L4 defect signal inverse |
| Final AQL + PSI | T-10 | 30-day RMA baseline | L4 defect signal inverse |
| Container consolidation + C/O | T-7 | NNN Tier-3 disclosure matrix signed | L5 IP compounding |
| FBA inbound booking + freight dispatch | T-5 | UN3481 freight booked | L1 lead time compounding |
| FBA inbound dock receipt | T-0 | ASIN live, Buy Box eligibility flag enabled | All 5 levers compounded |
Glossary
Key terms used in this guide:
- Buy Box
- The Amazon Buy Box is the featured offer on an Amazon product detail page that customers can add to cart with one click. Awarded based on a real-time scorecard the platform updates every 15 minutes.
- Buy Box Velocity
- The ratio of compounding 5 levers (FBA inbound lead time, sell-through velocity, price competitiveness, defect signal inverse, account health / IP) that determines how often the Buy Box is awarded to a given listing.
- Helium 10
- A suite of Amazon seller tools including Cerebro (demand-pool sizing), Magnet (cluster keyword discovery), Frankenstein (master-keyword list builder), Scribbles (live-index audit), and Index Checker (density audit).
- UN3481
- IATA DGR and 49 CFR classification for lithium-ion batteries contained in equipment, requiring SoC ≤30% for FBA inbound.
- Section 301
- USTR tariff schedule imposing 10-25% additional duty on China-origin goods. Vietnam-origin heated apparel may qualify for ATIGA/EVFTA/UKVFTA preference qualification, reducing the duty burden by 0-10%.
- Brand Registry 2.0
- Amazon's trademark-based brand protection program that unlocks A+ Content, Brand Store, Brand Analytics, Vine reviews, and the Brand-Registry-only Buy Box eligibility flag.
- IP67
- Ingress Protection rating indicating no dust ingress and no water ingress at 1m depth for 30 minutes. Verified by a 500V hipot sealing test.
- FMEA RPN
- Failure Mode and Effects Analysis Risk Priority Number, calculated as Severity × Occurrence × Detection. RPN ≥100 triggers a CAPA workflow.
- PPAP
- Production Part Approval Process, an 18-element documentation chain submitted to the customer before bulk production.
- AQL
- Acceptance Quality Limit, the statistical sampling standard for production QC. Typical AQL for heated apparel: 0.65 critical, 1.0 major, 2.5 minor.
12. Frequently Asked Questions (Engineering-Side)
**Q1. What is the BOM cost-engineering layer map for heated apparel at the Dongguan factory?**
The 8-layer map covers graphene yarn, carbon-fiber heating element, 21700 cell, BMS PCB + dual-branch firmware, lamination stack-up, outer shell, zipper + YKK trim, and packaging. Total BOM cost is $23.35/garment, landed FOB Vietnam $29.20/garment, landed DDP-FBA US $36.81/garment.
**Q2. What is the 21700 cell cycle engineering spec?**
The spec covers capacity retention ≥80% at 500 cycles, 0 cycle count pre-shipment, SoC ≤30% at FBA inbound, BMS handshake 4-state validation, cell vendor diversification (Samsung + LG + EVE), cell topology (1S2P or 2S1P), internal resistance ≤25 mΩ at 60% SoC, and per-cell voltage + capacity + IR forensics log.
**Q3. What is the BMS handshake 4-state validation?**
The validation protocol covers 4 states: idle (V ≤10 mA), heat-low (0.5A), heat-mid (1.0A), and heat-high (2.0A). The handshake bit is a 32-bit signature embedded in the BMS firmware that the engineering-side owner hashes at the firmware freeze stage (T-55 in the Q4 calendar).
**Q4. What is the dual-branch BMS firmware architecture?**
The architecture covers 25 kHz skiing + 31 kHz hunting dual-branch firmware, allowing the same Q4 hero-SKU to be sold across two use-case clusters. The firmware hash is the engineering-side source artifact for the supplier-side Brand Registry 2.0 9-artifact pipeline.
**Q5. What is the 8-layer lamination stack-up?**
The stack-up covers outer shell, fleece inner, heating element, insulation, reflective foil, lamination adhesive, graphene yarn layer, and inner liner. Each layer has a defect class (Critical, Major, Minor) that maps to the AQL sampling plan and the SPC Cpk ≥1.33 chart analysis.
**Q6. What is the SPC Cpk chart analysis?**
The chart runs every 4 hours during bulk production. Cpk ≥1.33 indicates 4-sigma margin; Cpk ≥1.67 indicates 5-sigma margin (the Q4 hero-SKU target). A Cpk drop below 1.33 triggers an out-of-control action (OCA) that pauses the production line.
**Q7. What is the IP67 hipot 500V sealing test?**
The test applies 500V AC across the heating element + outer shell for 60 seconds, verifying the insulation is intact. The test is followed by a 30-minute water immersion at 1m depth, then a post-immersion hipot. Pass criterion is leakage current ≤5 mA.
**Q8. What is the FMEA RPN ≥100 CAPA closure protocol?**
The protocol covers 8 failure modes (zipper misalignment, BMS handshake fail, 21700 cell SoC drift, graphene yarn layer separation, IP67 hipot insulation breakdown, outer shell seam failure, lamination adhesive failure, UN3481 hazmat SoC > 30%). RPN is Severity × Occurrence × Detection; RPN ≥100 triggers a CAPA workflow that closes within 48 hours (corrective) and 30 days (preventive).
**Q9. What is the NNN Tier-3 disclosure matrix?**
The matrix covers 3 tiers: Tier 1 (public, Brand Registry 2.0 9-artifact pipeline), Tier 2 (restricted, NNN agreement, BOM cost layer map), Tier 3 (confidential, NNN Tier-3 disclosure matrix, graphene fabric spec + dual-branch BMS firmware + 8-layer lamination stack-up + cell vendor cycle forensics).
**Q10. What is the engineering-side's role in the 60-day Q4 hero-SKU launch calendar?**
The engineering-side owner has direct line-of-sight into L1 (FBA inbound lead time compounding), L4 (defect signal inverse), and L5 (account health / IP compounding). The engineering-side artifacts (BMS handshake firmware hash, 8-layer lamination stack-up BOM, IP67 hipot 500V test, FMEA RPN ≥100 CAPA closure) feed the supplier-side Q4 launch calendar.
**Q11. What is the relationship between the BOM cost layer map and the Buy Box price competitiveness lever?**
The DDP-FBA price ($36.81/garment at the Q4 hero-SKU target) is the L3 Buy Box price competitiveness anchor. The engineering-side owner engineers the BOM layers (graphene yarn, 21700 cell, BMS PCB, lamination stack-up) to keep the DDP-FBA price ≤5% above the next-lowest Buy-Box-eligible offer.
**Q12. What is the graphene yarn layer's role in the NNN Tier-3 disclosure matrix?**
The graphene yarn layer is the most confidential layer in the 8-layer lamination stack-up. The yarn origin + the lamination parameter confidentiality + the graphene fabric specification are all Tier-3 information, accessible only to the Dongguan factory engineering-side owner. Any disclosure outside the Tier-3 envelope breaks the L5 IP compounding lever.
*Heated Apparel Amazon Buy Box Velocity 2026: Dongguan Factory Engineering Spec View* is part of the P#89 cycle 6 slot 9/10 pillar series. Companion pillars: P#86 supplier-side (imissky) Vietnam OEM Q4 launch calendar, P#86 wholesale buyer-retailer-side (gearplant) Buy Box velocity playbook. Internal link: /battery-heated-apparel-factory/. Author: graphene editorial team.
Leave a Reply